ManuFactoryIQ
BUILT FROM COMBINED FACTORY & TECHNOLOGY EXPERIENCE

Built on the Factory Floor. Engineered for the Real World.

We did not learn manufacturing from a requirements document. We learned it on shift — managing supply chain, inventory, quality, production and cross-functional projects, and absorbing the consequences whenever the process, the system and the physical reality did not agree.

ManuFactoryIQ is what we built afterwards, from the technology side: tailor-made applications that follow the way a plant already works, stay connected to the ERP in both directions, and leave an evidence trail an auditor can follow.

15 + yrs
Inside Plant Operations
10 + yrs
Building Digital Systems
7 modules
One Connected Platform
6 frameworks
Evidence Mapped To Clauses
OPERATIONAL REALISM
“We have sat on both sides of the table — first managing the operational problems, then building the technology that removes them.”
warning 15 YEARS MANAGING PLANT-FLOOR FRICTION

We Lived the Problems

PAIN POINTS

Every defect in a process or a system is paid for in shifts, scrap and expedited freight.

01

Material shortages discovered too late

Lines stalling because the kit was never verified as staged when the shift started.

02

Inventory records that do not match the floor

Phantom stock, untracked line-side buffers, and painful quarterly reconciliations.

03

Manual production and quality records

Clipboards, lost paper travelers, illegible signatures, end-of-shift transcription errors.

04

Disconnected ERP, spreadsheets and shop-floor systems

Islands of data that force every team to keep a second, offline Excel tracker.

05

Traceability gaps

No reliable way to say which supplier lot went into which finished serial number.

06

Audit evidence spread across several places

Filing cabinets, local drives and e-mail chains searched under time pressure.

07

Project delays without clear ownership

Cross-department bottlenecks hidden behind a static Gantt chart.

08

Reports that explain yesterday but cannot guide tomorrow

Metrics that arrive a day after the scrap was already produced.

task_alt 10 YEARS ARCHITECTING REAL-TIME SYSTEMS

Then We Built the Answers

WHAT WE BUILD

Designed to remove the friction without adding a second job to the operator’s shift.

01

Intelligent material planning

Consumption models with dynamic safety stock and supplier lead-time buffers.

02

Real-time inventory visibility

Barcode and RFID scanning at the physical point of change, not at the desk afterwards.

03

Digital production workflows

Rugged terminals, paperless travelers and step-by-step operator guidance.

04

Integrated quality and traceability

Unbroken genealogy back to heat numbers, lots, machine parameters and the operator.

05

Automated ERP transactions

Backflush, scrap and receipt postings written through the ERP’s own supported interfaces.

06

Audit-ready records

Immutable change history, version control, and a compliance dossier exported on request.

07

Project and resource management

Deliverables tied to real capacity, work orders and plant priorities.

08

AI-assisted reporting and decision support

Risk alerts and schedule suggestions before the bottleneck turns into downtime.

verified

"Software written by people who never had to explain a line stoppage solves the wrong half of the problem."

FOUNDATION & EVOLUTION

From Operational Friction to a Connected Plant
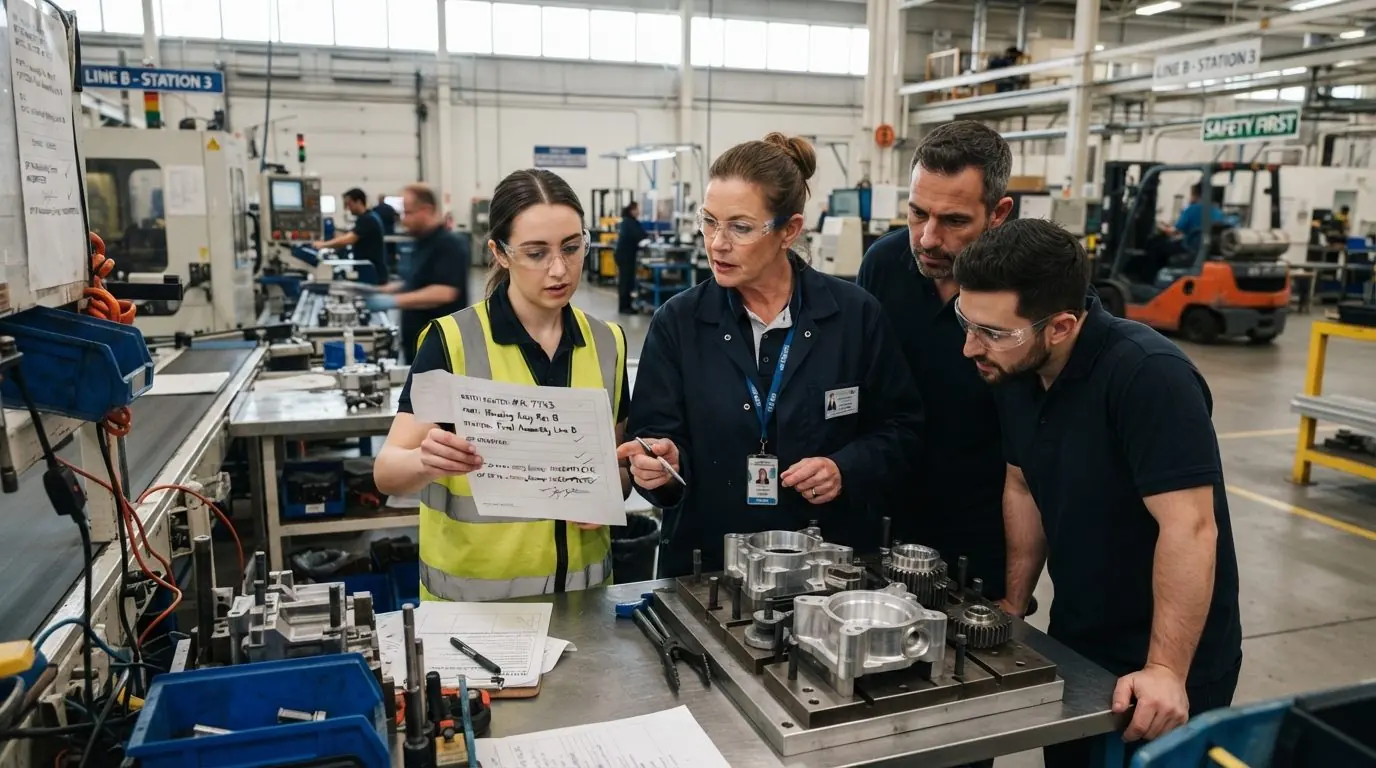
Cross-functional team at a machining line reviewing a checklist and machined housings on an inspection fixture
STAGE 01 factory

Working Inside the Operation

Years spent running supply chain, inventory, quality, production and cross-functional projects showed exactly where traditional systems give up.

Discovery: the disconnects cause the downtime
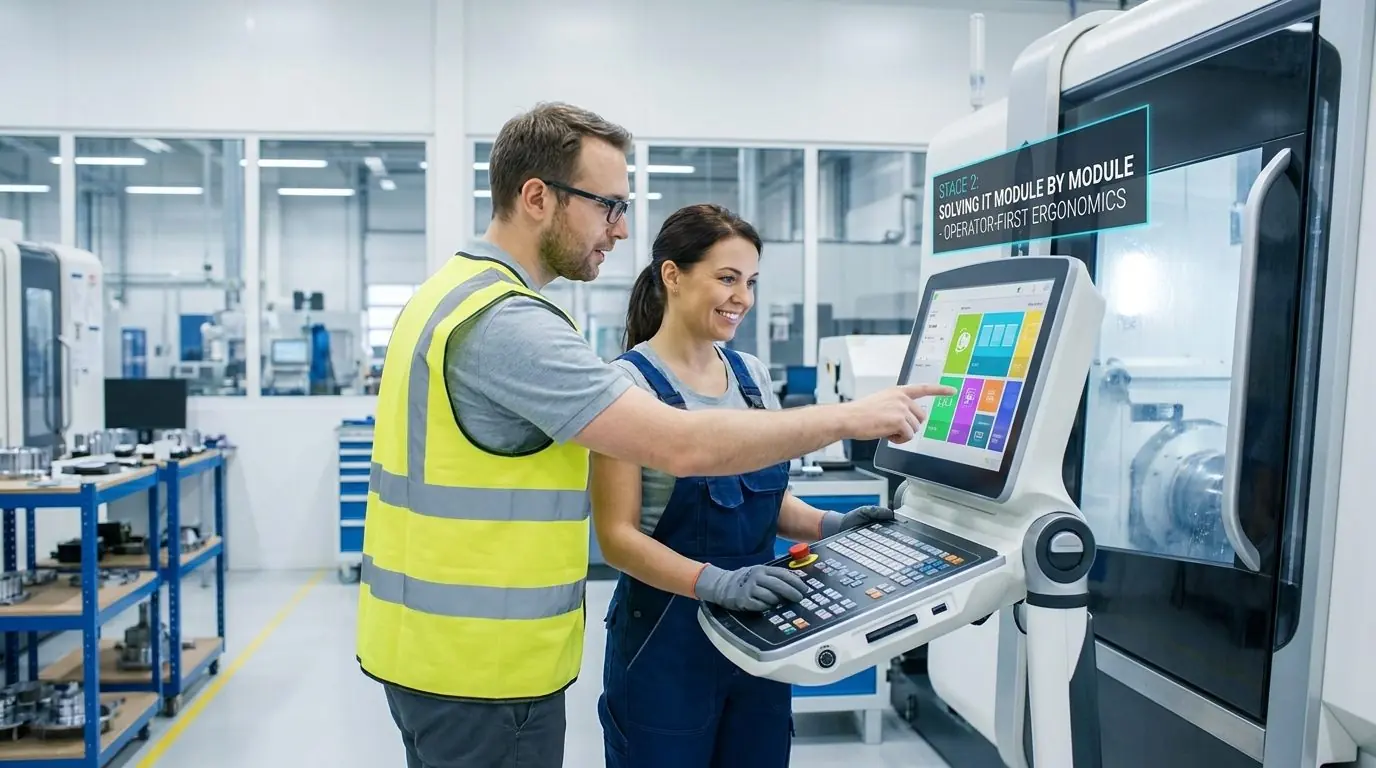
Supervisor in a high-visibility vest guiding a machine operator through a simple touchscreen application on a CNC machine terminal
STAGE 02 build_circle

Solving It Module by Module

Instead of asking teams to bend around rigid software, we built focused applications around the work that was actually being performed.

Strategy: operator-first ergonomics
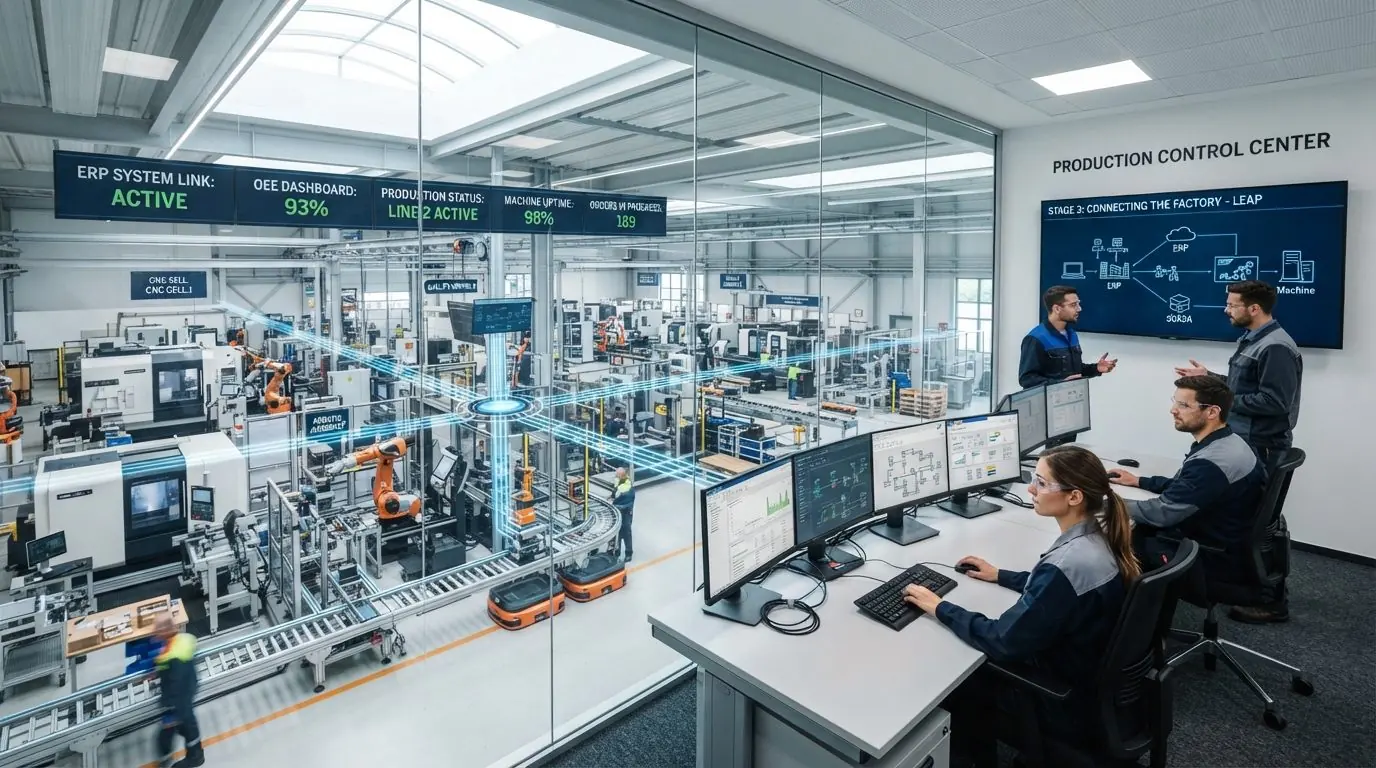
Production control center overlooking a connected machining floor, with engineers at monitors and a wall screen linking ERP, machines and operators
STAGE 03 schema

Connecting the Factory

Those applications grew into one platform that links people, processes, machines and the ERP instead of leaving each in its own island.

Leap: two-way ERP and machine data
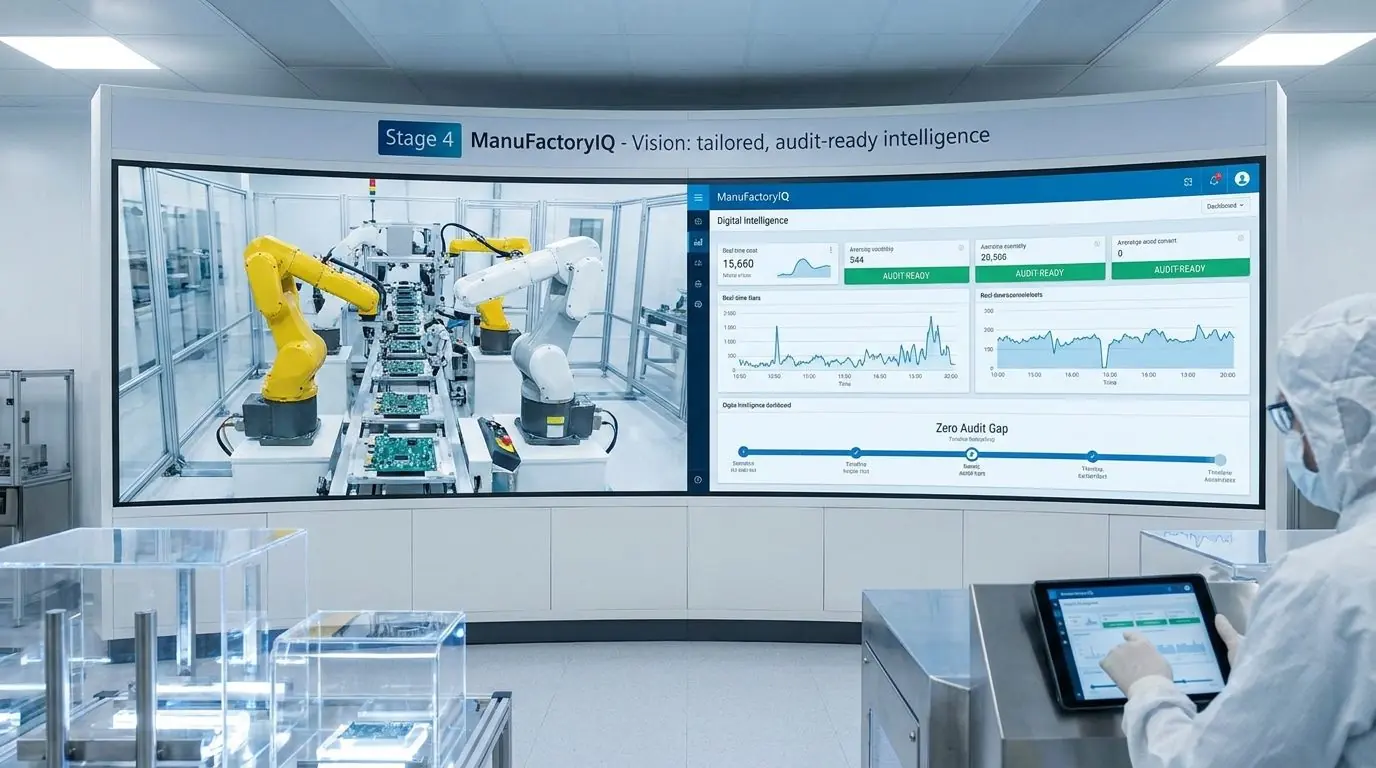
Cleanroom with a curved wall display showing robotic PCB assembly beside an audit-ready intelligence dashboard, and a technician in a cleanroom suit using a tablet
STAGE 04 cognition

ManuFactoryIQ

Today we deliver tailor-made digital manufacturing solutions that adapt to each plant’s operation — not the other way around.

Vision: tailored, audit-ready intelligence
DEEP INDUSTRIAL FLUENCY

We Know the Weak Points

Because we have personally managed every one of these failure modes on a live plant.

task_alt

"Nobody has to explain to us what a phantom stock figure or a missing traveler costs. We have paid for both."

PROCESS-FIRST METHODOLOGY

Your Operation Should Not Have to Adapt to the Software.

Every plant has its own products, processes, vocabulary, controls and constraints. That is why we start on the floor: we watch how the work really happens, map the physical process, mark the control points that matter, and build a one-to-one digital counterpart of the operation before a single screen is designed.

verified Part of the Workflow, Not Extra Work

The technology has to fall inside the movement the operator already makes. If it adds a step, it becomes another administrative burden and the data stops being true.

END-TO-END DIGITALIZATION PIPELINE

STEP 01

Observe the Real Process

visibility
STEP 02

Map People, Material & Controls

device_hub
STEP 03

Build the Digital Counterpart

view_in_ar
STEP 04

Develop the Tailored Application

terminal
STEP 05

Connect ERP, Machines & Data

sync_alt
STEP 06

Keep Improving With the Plant

trending_up
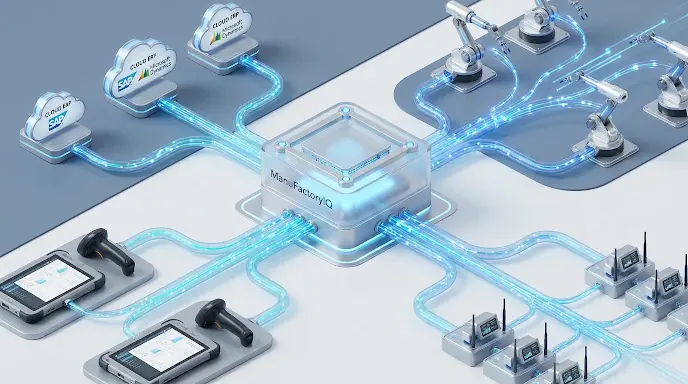
Integration layer connecting shop-floor machines, operators and enterprise systems
THE CONNECTING LAYER

Shop-Floor Reality, Written Back Into Enterprise Logic

Scans, machine signals and operator confirmations become ERP transactions in both directions — and each one keeps the record that proves where it came from.

See the integration architecture arrow_forward
REGULATORY INTEGRITY

Designed From a Lead Auditor’s Point of View

Compliance cannot be bolted on at the end of a project. ManuFactoryIQ is built with an understanding of what an auditor actually examines, which evidence carries weight, where process controls usually fail, and how a record has to connect from requirement to execution.

check_circle

Complete transaction and change history

Every scan, edit and system event logged with who, when and from which station.

check_circle

Role-based responsibility and approval

Authorisation matrices that stop a signature being given by the wrong discipline.

check_circle

Product and material genealogy

Parent-child tracking from incoming lot through to the shipped serial number.

check_circle

Controlled specifications and documents

Only the current revision reachable on the floor tablet — no obsolete prints in circulation.

check_circle

Inspection and test evidence

Gauge readings, tolerance checks and calibration certificates attached to the record.

check_circle

Nonconformance and corrective action

8D workflow, quarantine interlocks and root-cause verification kept in one chain.

check_circle

Training and competency checks

A station can refuse to start when the operator’s required qualification is not current.

check_circle

Version control and electronic approvals

Signature workflows designed around 21 CFR Part 11 expectations for electronic records.

check_circle

KPI-to-source traceability

Drill from a management metric down to the lot, shift or line event that produced it.

check_circle

Fast, organised evidence retrieval

Audit packets assembled from the live record instead of a search through cabinets and inboxes.

FRAMEWORKS THE PLATFORM IS BUILT TO EVIDENCE

ISO
ISO 9001 Traceability & CAPA
ISO
ISO 14001 Environmental records
IATF
IATF 16949 Automotive QMS
VDA - Verband der Automobilindustrie
VDA 6.3 Process audit
SAE International
AS9100D Aerospace & defense
U.S. Food and Drug Administration
21 CFR Part 11 Electronic records

ISO, IATF, VDA, SAE International and FDA names and marks are the property of their respective owners and are shown here only to identify the standards the platform is built to evidence. ManuFactoryIQ is a software provider, not a certification body, and these marks do not indicate certification or endorsement of ManuFactoryIQ or of your plant.

fact_check

"When an auditor asks a question, the answer should come from connected evidence — not a last-minute search through spreadsheets, e-mails and paper."

FOUNDATIONAL VALUES

How We Work

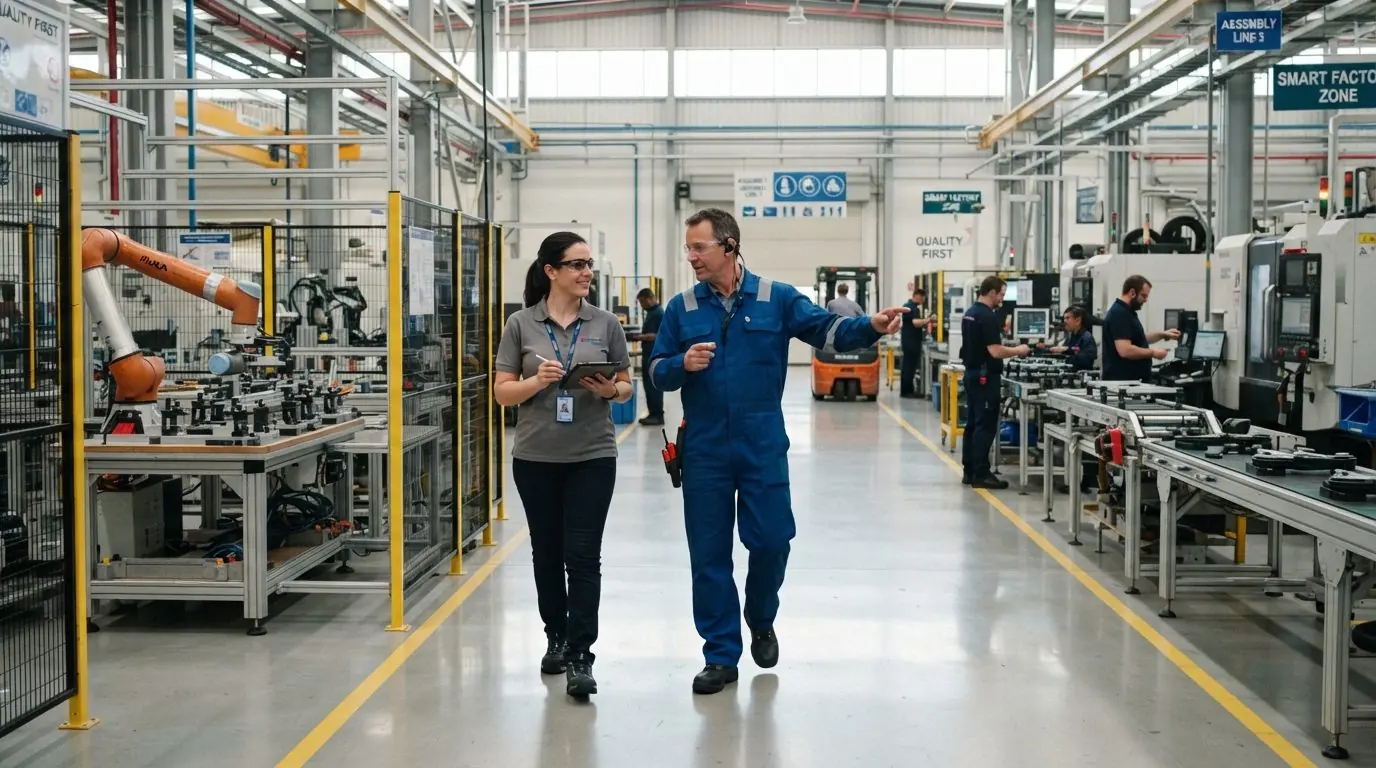
Process engineer with a tablet walking an assembly line with the line supervisor, reviewing the process in place
explore

Start on the Shop Floor

The real process is the starting point — not the software screen.

PRINCIPLE 01
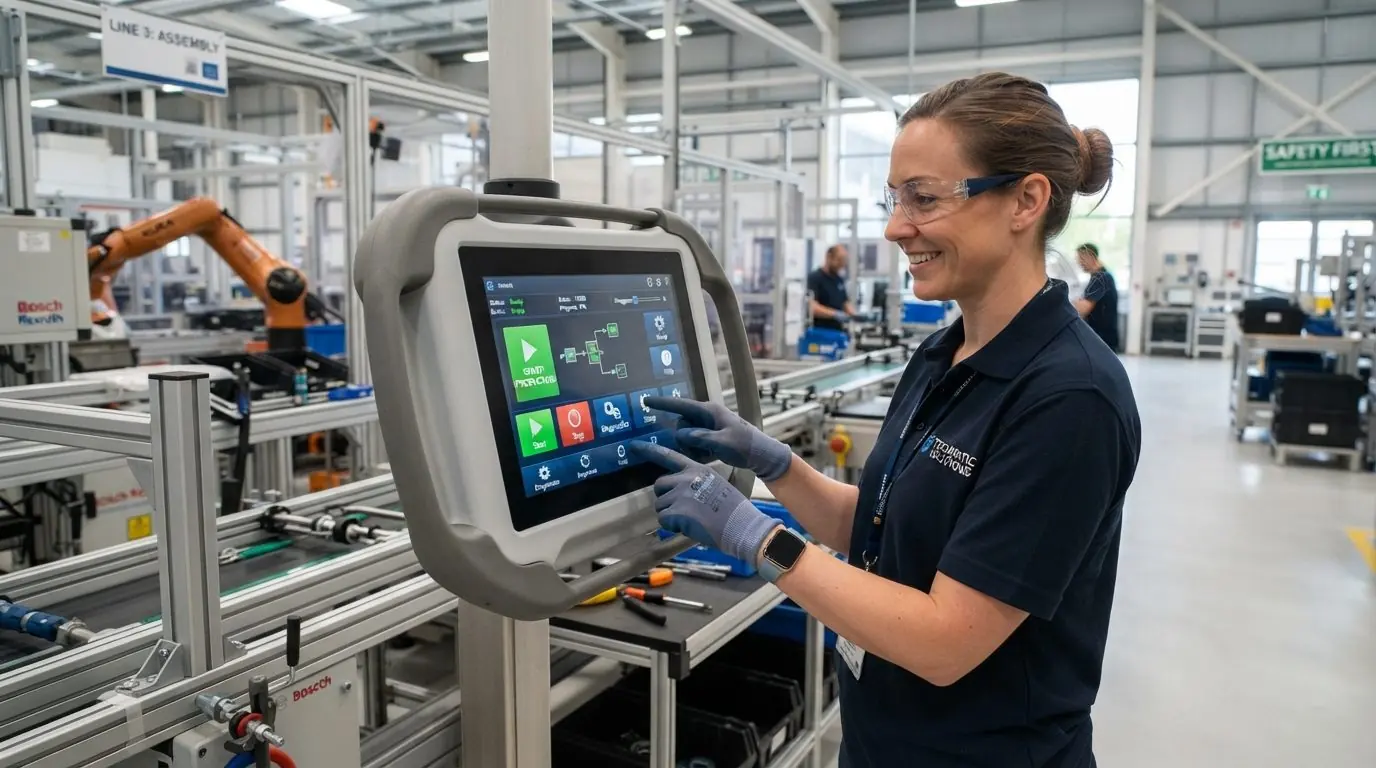
Operator in safety glasses and gloves confirming a step on a guided workstation terminal at an assembly line
groups

Fit the Technology to the People

A system should follow the natural workflow and make the correct action the easiest one.

PRINCIPLE 02
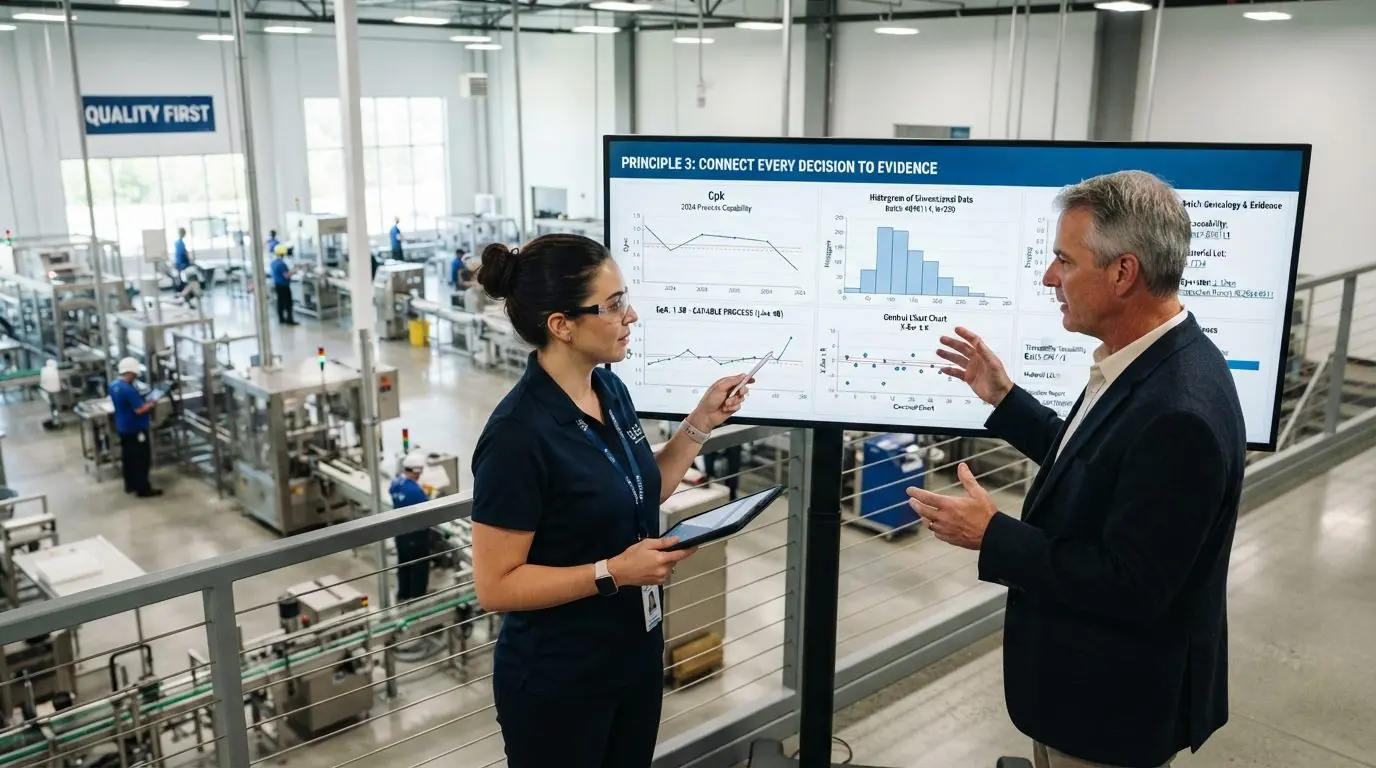
Quality engineer and plant manager reviewing capability charts and lot genealogy on a shop-floor dashboard screen
history_edu

Tie Every Decision to Evidence

Every KPI, alert and AI suggestion has to trace back to a source record someone can open.

PRINCIPLE 03
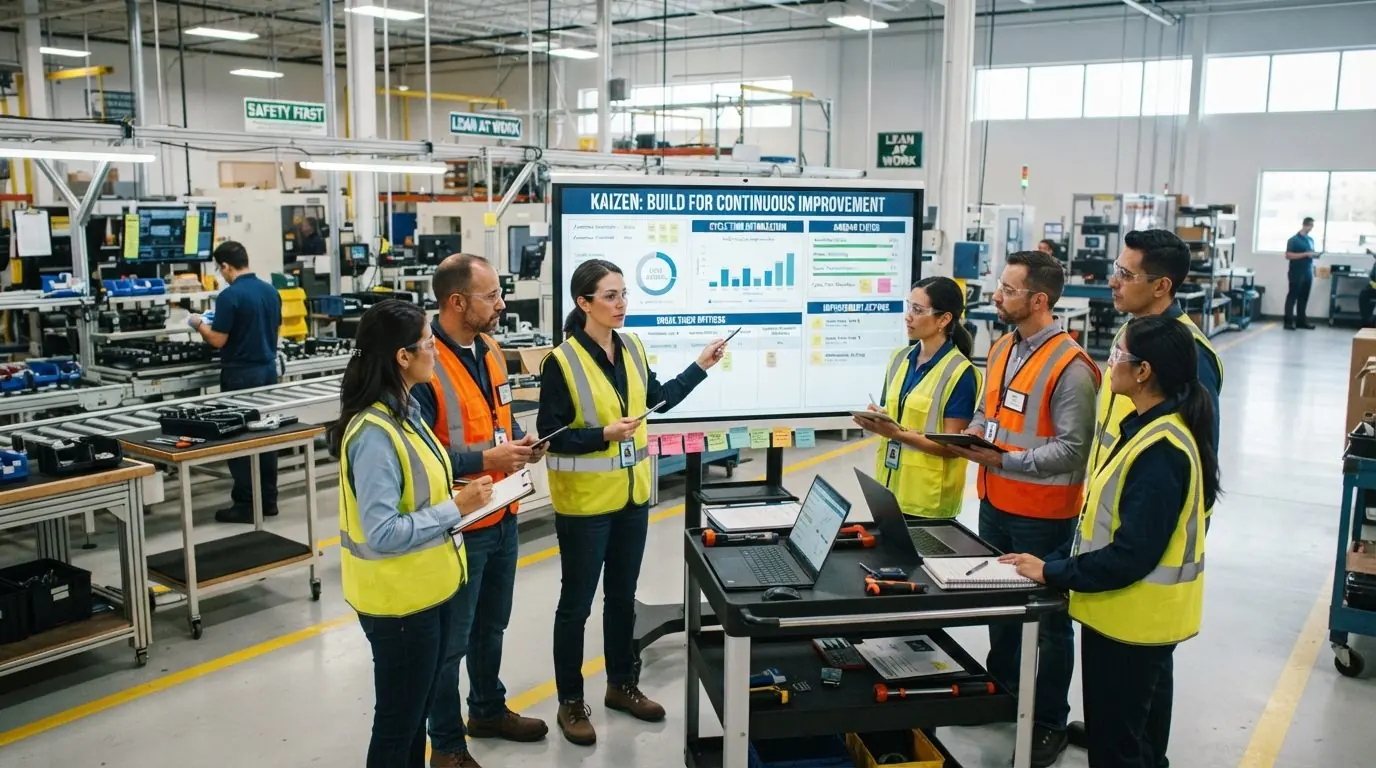
Improvement team in high-visibility vests standing around a shop-floor board, reviewing cycle-time and action items together
change_circle

Build for Continuous Change

The solution has to keep moving as the plant, the products, the customers and the priorities move.

PRINCIPLE 04
verified_user WE HAVE RUN THE OPERATION TOO

We Know Where Manufacturing Systems Break.

ManuFactoryIQ puts operational experience, digital transformation work, audit knowledge and modern AI into solutions shaped around the way your plant actually runs.

Show us how your operation works today — we will help you design what it looks like digitally.

FACTORY DISCOVERY SESSION

Tell Us How Your Plant Runs Today

A 45-minute conversation with people who have carried the same problems on a shift. We walk your process, mark the points where the data breaks, and show which part of the operation a tailored solution should cover first.

  • Walkthrough of your current process and its break points
  • Which module pays back first, and why
  • An integration path for the ERP you already run
“They asked about our staging area before they asked about our servers.”
— Operations Manager, Precision Components Plant
Strict enterprise NDA guaranteed. No invasive changes to your production ERP required.
Request a Demoarrow_forward